
Industrial High Temperature Heat Pumps for Food & Beverage Processing
A food plant does not have one heat demand — it has six, each at a different temperature, each served by a different piece of equipment, and each bounded by a food-safety rule you cannot negotiate with. Drag the slider below to match a heat pump series to your process, see which of the six HETAPRO machines fits, and find out where electrification genuinely beats a boiler — and where the boiler stays because the physics or the regulation says it must. No blanket payback promise: just the engineering boundaries and the numbers behind them.
From an 80 °C CIP wash to 150 °C UHT steam: a solution for every temperature we reach
Select the temperature your process actually needs. The panel below identifies the matching heat pump series, the realistic COP at that lift, the heat sources that can feed it, and whether a boiler still has a job to do. Drag, or use the arrow keys. The scale runs to 150 °C because that is the highest temperature any HETAPRO machine delivers — the 110–150 °C band is the HT steam series. Processes demanding more than that, such as spray-dryer inlet air at 150–220 °C, coffee roasting at 180–240 °C and tunnel-oven bake at 180–250 °C, are not on this scale because no machine in the range reaches them.
CIP cleaning and thermal sanitation — 80 / 85 °C
Every food plant runs a cleaning-in-place cycle, and it is the most reliably scheduled heat demand in the building: a fixed number of hours, every production day, at a temperature set by the microbiological specification rather than by the recipe. A typical plant runs clean-in-place at 80–85 °C, recirculated through tanks, pipework and plate heat exchangers, with the final rinse at a higher setpoint for product-contact surfaces. The heat is delivered as circulating hot water, which is exactly what a heat pump produces — no combustion, no flue gas, and no carbon particulate anywhere near food-contact surfaces. This is the natural first project on most sites because the load is continuous, the savings are immediate, and the food-safety argument is easier to make than a carbon argument.
Six industrial heat pumps, matched to your process and your available heat source
HETAPRO builds six high temperature heat pump machines: MT-W2W and MT-A2W (95 °C hot water), HT-A2W (135 °C hot water), HT-W2S and HT-A2S (110–150 °C saturated steam) and MT-A2A (30–85 °C hot air for drying). Which one is right for your food plant depends on two questions, not one: what temperature do you need, and what heat source do you actually have? Because a water-source machine and an air-source machine delivering the same 95 °C are different machines with different economics. The cards below are ordered by delivery temperature; the recommended one for your selected temperature band is highlighted.
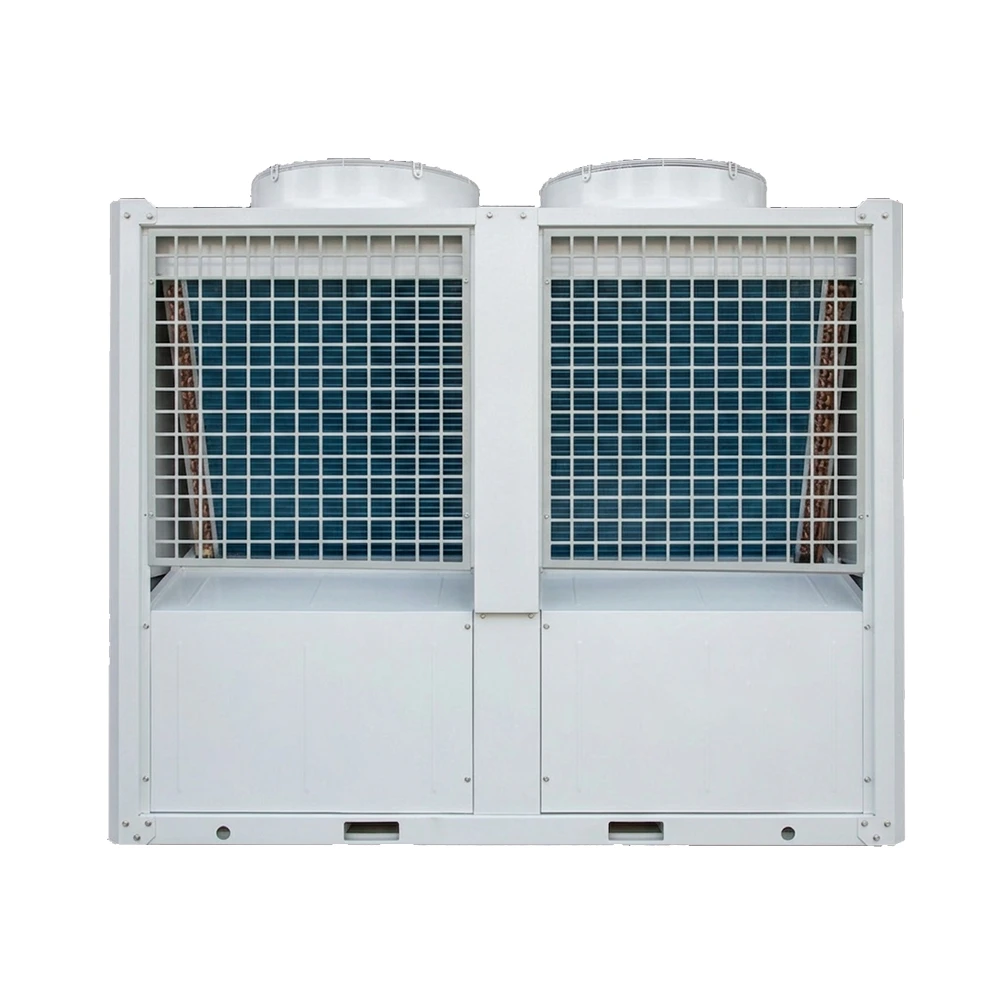
The workhorse of the low-temperature end of a food plant. An air-source high temperature heat pump using ambient air as the heat source, producing hot water up to 95 °C for plant hot water, wash and rinse circuits, jacket heating and boiler feedwater preheat. Where a plant has no recoverable waste hot water at all — a greenfield site, a plant whose condensate is already committed elsewhere — this is the machine that will run, because it needs nothing from the process. Scroll compressor, VFD driven, weather-independent at the coldest hours of a tropical or temperate night, and it displaces a boiler that was otherwise firing 3,000 hours a year to do exactly this job.
- CIP and thermal-sanitation hot water supply
- Plant hot water, wash and rinse circuits
- Jacket heating for tanks, kettles and vessels
- Boiler feedwater preheat
- Low-temperature pasteurisation loops
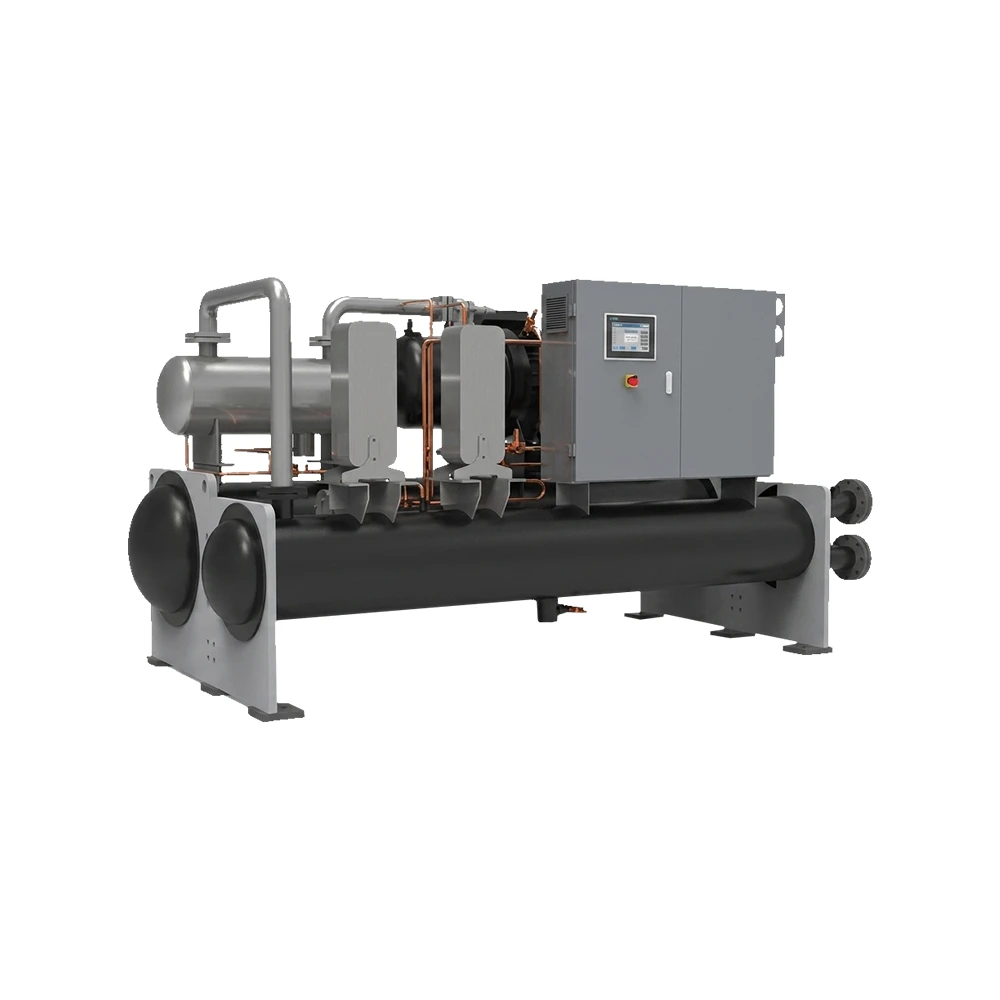
The most capable machine in the range for a plant that has recoverable hot water, and the one most food processors specify first. A screw compressor with VFD lifts low-grade heat from water source to 95 °C circulating hot water. Every food plant with a boiler has a condensate return: typically 60–52 °C at the point of collection, and typically returned to the feedwater tank at a loss. Close the loop properly and this machine runs at COP well above what any air-source unit can reach, on the hottest ambient day of the year, with no degradation. It is the machine that turns a CIP system or a rinse-water circuit from a cost centre into a heat source.
- CIP and thermal-sanitation hot water supply
- Condensate recovery and boiler feedwater preheat
- Jacket heating and vessel make-up
- Continuous base load on a plant header
- Effluent heat recovery at 30–50 °C

A reciprocating-piston compressor raises ambient air to 135 °C of pressurised hot water. This is the machine for the duties a scroll unit cannot hold: high-temperature rinse circuits, thermal-sanitation regimes that specify 90–95 °C water at the nozzle, and the warm side of a vacuum evaporator's secondary circuit. It sits awkwardly in a food plant for one reason and one reason only — 135 °C is above the point where you would ever put it in contact with product. Its real value in F&B is as a utilities machine: heating the hot-water header, the wash-down circuit and the boiler feed tank, so the boiler spends its fuel on product-contact duties where the temperature genuinely matters.
- High-temperature wash and rinse circuits
- Thermal sanitation above 90 °C
- Hot-water header for the plant
- Boiler feedwater preheat at temperature
- Preheat for a downstream steam generator
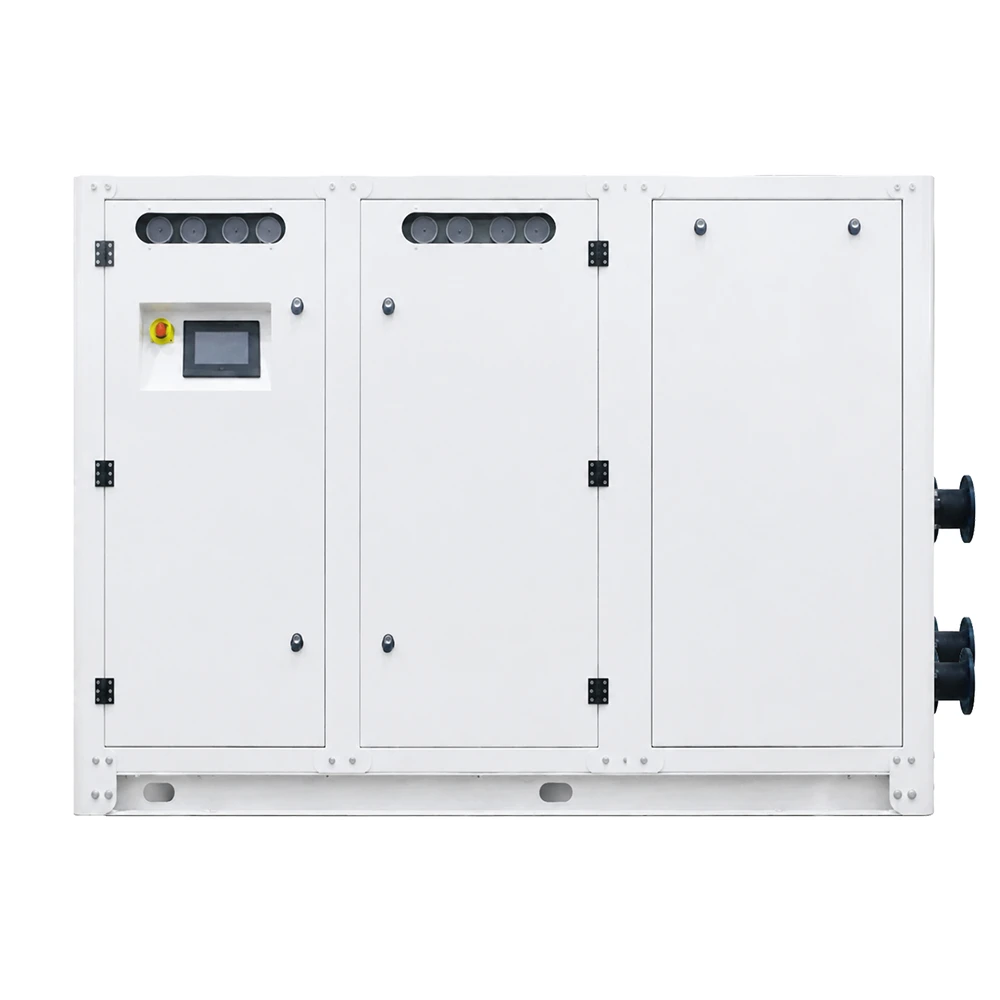
Turns 55 °C-plus waste hot water directly into 110–150 °C saturated steam. This is the machine that changes the conversation in a food plant, because a large share of a beverage or food plant's steam demand is not product-contact at all — it is the plant's central steam header serving CIP, tank heating, jacket circuits and general process. A high-efficiency single-stage compression system built for plants that have both significant waste hot water and a live steam demand. In a juice or dairy plant the evaporator condenser and the pasteuriser condensate give you exactly the source this machine wants.
- Central steam header for CIP and utilities
- Batch steam for cooking, blanching and boiling
- Steam make-up against an existing boiler load
- Evaporator heating in a concentration plant
- Preheat before a high-pressure steam duty
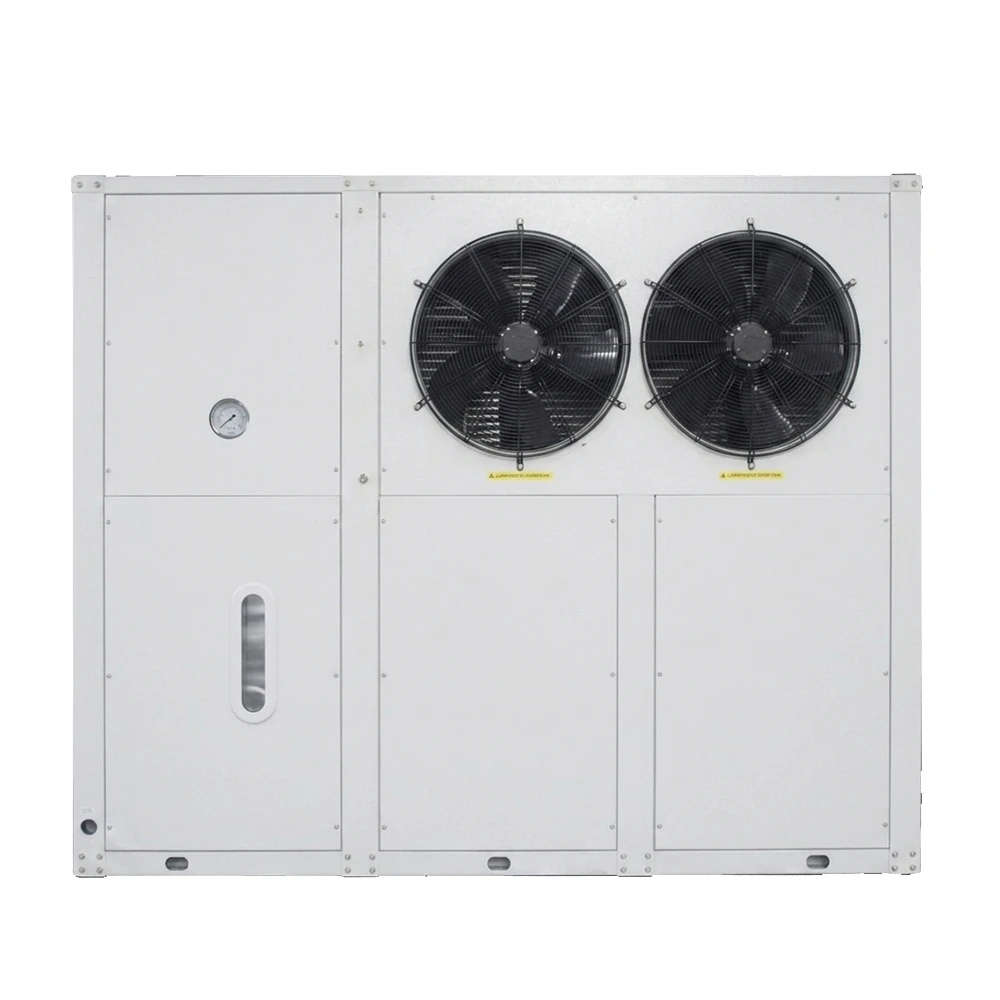
The same 110–150 °C saturated steam output as HT-W2S, but drawing on waste hot air rather than waste hot water. Where a plant has hot exhaust air — from a spray dryer, a tunnel dryer, a kiln, a refrigeration plant's condenser bank or an air-handling process — this is the machine that converts that air into usable steam for the plant's central header. In a fruit-juice, coffee or milk-powder plant the dryer exhaust is typically the largest hot-air stream on site and is usually discharged. Recovering it into process steam is one of the cleanest wins available in the sector.
- Steam from dryer or kiln exhaust air
- Central steam header for utilities
- Boiler load displacement at peak
- Batch steam for cooking and blanching
- Condenser-bank heat recovery

Not a hot water machine but a hot air machine. MT-A2A delivers 30–85 °C supply air for industrial drying, using ambient air or recoverable waste hot air as the heat source, and it runs weather-independent — the inverter compressor modulates output to the drying curve rather than cycling on and off. In food and beverage this is the machine for low-temperature drying: fruit and vegetable pieces, herbs, spices, seeds, coffee bean drying after wet processing, pasta, snack product, and any tunnel or belt dryer that currently runs on a gas burner at 60–80 °C. It is also the recovery machine that captures the hot exhaust of a spray dryer and returns it as process air.
- Tunnel and belt dryers at 60–80 °C
- Fruit, vegetable, herb and spice drying
- Coffee, cocoa and nut drying
- Spray-dryer exhaust heat recovery
- Dehydration of high-value products
| Model | Heat source | Source temp. | Output | Form | Compressor | Max unit | Food & beverage duty |
|---|---|---|---|---|---|---|---|
| MT-A2W | Ambient air | ≥10 °C | 95 °C | Hot water | Scroll | 350 kW | CIP, wash water, plant hot water |
| MT-W2W | Water / waste heat | 60/52 °C | 95 °C | Hot water | Screw + VFD | 1500 kW* | CIP, condensate recovery, feedwater preheat |
| HT-A2W | Ambient air | 55–85 °C | 135 °C | Hot water | Piston | 220 kW | High-temp rinse, hot-water header |
| HT-W2S | Waste hot water | ≥55 °C | 110–150 °C | Saturated steam | Single-stage | 500 kW | Steam header, batch steam, evaporator heating |
| HT-A2S | Waste hot air | ≥55 °C | 110–150 °C | Saturated steam | Single-stage | 220 kW | Steam from dryer exhaust air |
| MT-A2A | Air / waste hot air | 0–80 °C | 30–85 °C | Hot air | Inverter | 300 kW | Tunnel drying, low-temp dehydration |
A high temperature heat pump covers process heat up to 150 °C. It does not cover spray-dryer inlet air at 150–220 °C, tunnel-oven and baking duty at 180–250 °C, coffee roasting at 180–240 °C, or cocoa roasting above 150 °C. Nor does it replace a high-pressure retort in a plant whose product specification demands a validated 121 °C profile with the same dwell-time precision all year. Any supplier who tells you a heat pump covers a 200 °C oven is describing a different machine. Plan the boiler around those duties and electrify everything underneath them — that is where the tonnage and the savings are.
Does the heat pump actually beat the boiler on your site?
Two sliders, two formulas, no opinion. Set your own energy prices and boiler efficiency — the answer updates live. Use it as a screening test, then confirm with a proper audit.
Boiler heat cost = fuel price ÷ boiler efficiency · Heat pump heat cost = electricity price ÷ COP · Break-even COP = electricity price ÷ boiler heat cost. If your break-even COP is below what the series can deliver at your temperature, the project works on energy cost alone — before grants, carbon value or brand incentives.
What an industrial high temperature heat pump is — and what it is not
An industrial heat pump (IHP) is a vapour-compression machine that moves heat from a low-temperature source to a higher-temperature sink using an electrically driven compressor. Instead of burning fuel to create heat — where an electric boiler achieves an efficiency of 0.97–0.99 and a gas boiler 0.88–0.92 — the heat pump moves heat that already exists on your site and delivers it at the temperature your process needs.
For a food plant this matters in a specific way. Food and beverage is one of the few industrial sectors where cooling and heating are required at the same time, in the same building, on the same schedule. A dairy plant chills milk to 4 °C in the morning and heats wash water to 85 °C in the afternoon. A brewery cools wort from 100 °C down to 12 °C and then needs steam to boil the next batch. A fish plant runs a blast freezer at −35 °C and a CIP circuit at 85 °C. The heat that a freezer or a chiller has to dump is usually dumped into the sky. A heat pump recovers it and puts it back into the plant as usable process heat.
Three things this page will not do, because they damage more engineering trust than they win commercial interest.
We will not claim to replace the boiler
Industrial heat pumps are commercially proven up to about 120 °C for hot water and into the 150 °C range for saturated steam, but they are not scaled like boilers. Industry survey work finds the average steam boiler in a textile or food plant is an order of magnitude larger than the largest commercial steam heat pump. Whole-facility electrification is not a realistic proposition this decade. The bankable pattern is partial electrification: the heat pump carries the base load, the boiler becomes the peaking and standby unit. In practice that means the boiler fires less, wears less, and lasts longer — which is a better outcome than a brochure promising it can be deleted.
We will not claim to reach 200 °C
A heat pump delivering 200 °C is not a product today; it is a research target. Spray-dryer inlet air at 150–220 °C, tunnel-oven bake at 180–250 °C, coffee roasting at 180–240 °C, continuous frying at 160–190 °C and edible-oil deodorisation at 240–260 °C all sit above what any machine on the market can deliver. These duties keep their burners. What we can do is recover the exhaust air from those very processes — and a spray dryer running at 200 °C in and 85 °C out is discarding roughly a third of its energy in the flue.
We will not call it zero-carbon
A heat pump eliminates Scope 1 emissions at the plant — no stack, no NOx permit, no fuel storage, no flue-gas compliance. Scope 2 emissions move to the electricity supplier, they do not disappear. On a coal-heavy grid that is a genuine trade-off, not a win: in a 700 gCO₂/kWh grid the electricity route can carry more carbon than a gas boiler. Where the grid is clean — Brazil at 110 g, Chile at 289 g, Vietnam at 461 g — the case is decisive. Where it is not, the honest framing is "we removed your Scope 1, and here is what your Scope 2 looks like".
The six process series, and the machine behind each
These six series describe the process bands in a food and beverage plant. Each one is served by one or more of the six HETAPRO machines in the recommended machines section above — the series tells you what the duty is, the machine tells you what to buy.
Utility & Wash Water — 30 / 60 °C
The base layer. Wash water, rinse water, bath and make-up water, general plant hot water, boiler feedwater preheat. It runs at the highest COP of any series, which makes it the quickest-payback machine in the portfolio and the natural first stage of any phased project. Sourced from effluent and condensate return where available, ambient otherwise.
Machines: MT-W2W (water source, screw — first choice where waste heat exists) · MT-A2W (air source, scroll) · MT-A2A (hot air for drying)
Pasteurisation & Heating — 60 / 80 °C
Low-temperature and high-temperature short-time pasteurisation side circuits (63 °C for 30 minutes, 72–85 °C for 15–30 seconds), tunnel pasteuriser water loops, fruit and juice preheat, fermentation heating and general vessel jacket heating. This is the largest continuous hot-water load in a dairy, juice or brewery, and it sits almost exactly in the sweet spot of a high temperature heat pump.
Cleaning & Sanitation — 80 / 85 °C
CIP is the most reliably scheduled heat demand in any food plant, and in many plants it is the single largest: caustic wash at 70–85 °C, thermal disinfection and final hot rinse at 85 °C and above, recirculated at flow rates above 1.5 m/s through tanks, plate exchangers and spray towers. The heat is delivered as circulating hot water — which is exactly what a heat pump produces. No combustion, no stack, no particulate anywhere near product-contact surfaces.
Machines: MT-W2W — the single best first project on most food sites
Cooking, Blanching & Batch Steam — 85 / 100 °C
Blanching at 90–105 °C for fruit and vegetables, batch cooking, pan boiling, syrup boiling, steam for tank and jacket heating, and the plant's central low-pressure steam header. At the top of the comfortable band a buffer vessel is normally required so the machine can ride through batch gaps without the boiler trimming the header. A retained boiler becomes a peaking unit rather than the base load.
Machines: HT-W2S · HT-A2S (110–150 °C steam) · HT-A2W (135 °C hot water) · MT-W2W (95 °C base + buffer)
Evaporation, Concentration & Indirect Sterilisation — 100 / 130 °C
Second and third evaporator effects, vacuum-pan heating steam at 105–120 °C, syrup and juice concentration, and the superheated-water side circuits of indirect UHT and aseptic systems. COP falls to 2.2–2.9 here and the machine becomes a specialist. The first effect of a multi-effect evaporator runs at 65–75 °C and is continuously loaded — that is the best-shaped heat pump duty in the sector, and it is routinely overlooked because plant teams look at the whole evaporator rather than at its first effect.
High-Temperature Steam — 130 / 150 °C
Pressurised hot water at 135 °C, saturated steam at 130–150 °C, and the indirect thermal processes that sit at the top of our range. Here COP falls to 1.5–2.2 and the machine is a specialist, not a commodity. 150 °C is the ceiling of the entire HETAPRO range. Retort sterilisation at 121 °C is a separate argument: it stays with the boiler not because of temperature but because it needs pressurised saturated steam, and no industrial heat pump in this class provides that reliably.
Every series can be fed six ways
(1) CIP effluent and cooling-water bleed at 30–50 °C — largest volume, cleanest; yields COP 5 and above through a heat exchanger. (2) Condensate return above 80 °C — every boiler plant has one and most return it warm; closing the loop properly removes a large part of the feedwater heating load. (3) Flash and secondary steam at 105–120 °C — effectively free at the point of generation, and the evaporator is the best source on site. (4) Dryer exhaust at 80–120 °C — a spray dryer or tunnel dryer exhaust is usually discharged; recovered, it becomes steam or process hot water. (5) Refrigeration condenser heat at 40–60 °C — the cold chain in the same building, running continuously, with nowhere to put its heat. (6) Ambient air — the fallback when no better source exists.
Source decides the model: water above 55 °C → MT-W2W / HT-W2S · waste hot air → HT-A2S · ambient only → MT-A2W / HT-A2W
The four processes that decide the project
Most food plants carry four heat duties that, taken together, are the whole commercial conversation. Two are straightforward wins. One is the single best opportunity in the sector and is routinely overlooked. One is the hard boundary you need to write into the project scope on day one.
Clean-in-place — the entry point, every time
Caustic wash at 70–85 °C, acid wash at 60–80 °C, thermal disinfection and final hot rinse at 85 °C and above, recirculated above 1.5 m/s through tanks, plate heat exchangers and spray towers, with coverage typically verified by riboflavin UV testing. This is the largest and most predictable single hot-water load in a food plant, and it runs on a fixed schedule every production day — which is exactly the load profile a heat pump is built for. A 20,000 litre-per-day dairy running HTST, CIP and bottle washing together has been measured at roughly 11,400 kg of LPG per year for those three duties alone.
Machine: MT-W2W (water source) where condensate is available, otherwise MT-A2W
Pasteurisation — the side circuit, not the vessel
Low-temperature pasteurisation is 63 °C for 30 minutes; high-temperature short-time is 72–85 °C for 15–30 seconds; ultra-pasteurised is 85–90 °C for 8–15 seconds. The regenerative section of a plate heat exchanger can already recover 90–94 % of the energy — so the real question is what supplies the make-up. That make-up is hot water at 60–90 °C, which is a heat pump's best work. This is no longer a speculative application: a packaged dairy equipment major launched an integrated heat pump pasteurisation system in late 2025, reporting that a typical 60,000 litre-per-hour line running 6,000 hours a year cut operating cost to about €230,000 and reduced CO₂ by up to 650 tonnes per year.
Evaporation — the best-shaped load nobody counts
Multi-effect evaporation is where the numbers get serious. A single effect consumes roughly 1.1–1.2 tonnes of steam per tonne of water evaporated; five effects consume 0.24–0.30. Take a dairy evaporating 18,750 kg of water per hour from 12 % to 48 % total solids: at a three-effect steam economy of 2.5 that is about 7,500 kg of steam per hour. The first effect runs at 65–75 °C, continuously, and is the best-shaped heat pump load in the entire sector — comfortable temperature, steady draw, and it is usually overlooked because plant engineers look at the evaporator as one unit rather than at its first effect. Note that mechanical vapour recompression is a competing route on the same duty, not a complement: decide which one owns the evaporator before you scope the heat pump.
Machine: MT-W2W for the first effect · HT-W2S for second and third effect steam
Drying — we take the exhaust, not the burner
A spray dryer running 200 °C inlet air and 85 °C outlet air has a thermal efficiency of roughly 65 %; the rest leaves in the exhaust. The inlet air is above any heat pump and stays on gas. But the exhaust carries moisture, and condensing that moisture and re-heating it is a clean, cheap recovery that industry has been doing with heat pumps for years. For low-temperature drying the picture is simpler: tunnel and belt dryers at 60–90 °C for fruit, vegetables, herbs, spices, coffee, cocoa and pasta are directly within reach of the 85 °C hot-air machine, and food-industry guidance has long advised replacing steam with hot water in these applications because a heat pump system is simpler, cheaper and has a higher COP.
Machine: MT-A2A (30–85 °C hot air) for drying and exhaust recovery · HT-A2S for steam from exhaust air
A high temperature heat pump covers process heat up to 150 °C. It does not cover spray-dryer inlet air at 150–220 °C, tunnel-oven and baking duty at 180–250 °C, coffee roasting at 180–240 °C, continuous frying at 160–190 °C, or edible-oil deodorisation at 240–260 °C. Nor does it replace a high-pressure retort in a plant whose product specification demands a validated 121 °C profile: that is a pressure requirement as much as a temperature one, because the retort needs pressurised saturated steam that no industrial heat pump in this class provides reliably. Any supplier who tells you a heat pump covers a 200 °C oven, or a retort, is describing a different machine. Plan the boiler around those duties, and electrify everything underneath them — that is where both the tonnage and the savings are.
Commercial sterility for low-acid foods is defined in the United States by a time–temperature integral, F₀, referenced to 121.1 °C. The definition is about the curve the product experiences, not about where the heat came from — a valid F₀ can be delivered by any source that achieves the profile. The reason a retort stays on the boiler is narrower and harder: it operates under pressure with saturated steam as the heating medium, and industrial heat pumps at this class deliver hot water or superheated steam, not reliably pressurised saturated steam at the right quality and the right rate. The realistic partial substitution is everything around the retort: CIP cleaning, pre-rinse water, jacket preheat, basket and tray washing — which together are a substantial share of the steam load on a canning line.
Five recoverable heat streams, and the order to recover them in
| Source | Typical temp. | Delivers | Constraint |
|---|---|---|---|
| CIP effluent / cooling-water bleed | 30–50 °C | Hot water 60–95 °C at COP 5+ | Filtration, pump cavitation control; fouling on plate exchangers |
| Condensate return | > 80 °C | Hot water 95 °C and feedwater preheat | Only as good as the return network; oil and sugar contamination |
| Flash / secondary steam | 105–120 °C | Saturated steam 110–150 °C | Pressure matching; must not disturb the evaporator balance |
| Dryer / oven exhaust air | 80–120 °C | Steam or hot water for the header | Moisture, particulate and product residue; washable surfaces required |
| Refrigeration condenser heat | 40–60 °C | Hot water 60–90 °C, CIP and pasteurisation | Run-time coupling to the cold load; needs thermal storage |
| Ambient air | ≥ 10 °C | Hot water 95 °C / hot air 85 °C | Site ambient profile enters the COP; hot climates hurt |
Read this before quoting a payback number
Published industrial heat pump case studies report payback periods from under six months to eight years. That range is not noise — it is the ratio of your fuel price to your electricity price, and the availability of recoverable waste heat, doing all the work. Two independent reference points from the same body of work: a Ukrainian brewery installing a 1.5 MW system reported total energy down 75 %, and a UK brewery funded by the government energy accelerator and independently verified by the Carbon Trust reported 86 % energy reduction on the boiling stage alone at a coefficient of performance near 6. Both projects had a heat source worth recovering.
A plant with no waste heat and a cheap gas boiler is a different project. We will say so during the audit rather than after the purchase order — and where that turns out to be the answer, the meter-and-control work we recommend first usually pays back faster than we do.
There is a class of project where a heat pump is not replacing a boiler, it is replacing the fuel a boiler burns, while the boiler stays as the peaking and standby unit. UNIDO's Industrial Energy Systems branch is running exactly that demonstration in South Africa: its "Coal Zero by Green Steam" project at a food processing plant pairs solar thermal collectors, a high-efficiency mechanical vapour recompression heat pump, waste heat recovery and a digital twin, with the plant paying for steam on a service basis rather than buying the equipment. The stated objective is around 2,754 tonnes of CO₂ equivalent avoided a year and more than four tonnes of coal out of use each day, and the design is modular — more collector rows or storage can be added as the steam demand grows.
The transferable part is the method, not the machine: a heat pump, a complementary heat source, storage and digital control working together under a performance guarantee, with the boiler kept as standby. Where your duty sits above 120 °C, the same architecture applies with a high-temperature steam machine at its centre — the heat pump carries the base load, the boiler covers the peaks, and nothing has to be deleted.
Who we are looking for
This page is written for the people who actually specify and install the equipment, not for the end customer's procurement department. Specifically:
EPC and system integrators
Firms who design and build food and beverage process plants, or who retrofit utilities to an existing plant. You need a manufacturer who will hand you a machine, a control architecture, a buffer vessel strategy and an electrical scope — and who will co-ordinate with your own mechanical and electrical contractors rather than around them.
Chiller engineering contractors
Anyone already selling and servicing Midea or Gree industrial chillers into food plants is, functionally, already selling cold-side equipment with the same service culture, the same customer and often the same maintenance contract. If you can install and maintain an ammonia or screw chiller, you can install and maintain a high temperature heat pump — and the plant that buys the chiller is the plant that needs the hot side.
Boiler dealers and service providers
The firms who own the service relationship with the boiler are the ones who hear about a failed boiler first. We are not asking you to sell something that replaces your product — we are asking you to sell the machine that takes the base load, makes your boiler a standby unit, and extends its life. That is a conversation you can have with a customer you already have.
Engineering departments of very large plants
Multi-site groups with their own energy and utilities teams — dairy groups, brewery groups, coffee roasters, sugar and edible-oil refiners, poultry slaughterhouses. They write specifications, they run tenders, and they measure payback against a corporate hurdle rate. Give them the boundary conditions and the physics; they will do the arithmetic themselves.
Utilities and steam plant operators
In industrial parks where the steam is produced centrally and sold to tenants, the economics live at the plant level, not the tenant level. An industrial park steam operator can electrify its own boiler house once and sell lower-carbon steam to every food tenant on the site.
What we need from a partner
Local installation and commissioning capability, a genuine service and spares commitment for a machine that runs 6,000 hours a year, and an engineering team willing to start the project with a metering exercise rather than a price list. If you can commit to those three things, we can commit to a technical scope, a guaranteed COP at your duty point, and an electrical and mechanical scope priced up front.
How we deliver it

High temperature heat pumps are not plug-and-play. Poor system design produces oversized equipment, underperforming assets and damaged confidence in the technology. Our sequence is deliberately conservative.
Level-1 energy survey and metering
Twelve months of fuel and electricity bills, steam header pressure and temperature profiles, flow rates on CIP and pasteuriser circuits, production schedule by product, evaporator duty, dryer exhaust temperatures, and the actual condensate return practice. We size against your real load profile, not a rule of thumb per tonne of product. Where a unit already runs below benchmark, we will tell you that metering and control work pays back faster than we do — and we will say so in writing.
Thermal, electrical and control design
Heat source identification across all five streams, sink temperature definition per process, buffer vessel and thermal storage strategy, transformer and switchgear assessment, harmonics and voltage-drop review, and the hygienic specification for every wetted surface. We state the electrical and mechanical infrastructure scope explicitly in the quotation, because this is where industrial heat pump projects most often go wrong. HETAPRO machines are supplied for 380–415 V, 3-phase, 50 Hz as standard, with 60 Hz versions available, and the control architecture is PLC with HMI, high/low pressure and overload protection plus remote monitoring.
Staged installation
Stage 1 — condensate and effluent heat recovery plus feedwater preheat, which runs at COP 5+ and needs minimal lift. Stage 2 — the heat pump covering CIP, pasteurisation and blanching, at the point of use, with a buffer vessel. Stage 3 — steam generation at 110–150 °C for the plant header, with the boiler retained as the peaking and standby unit. Each stage stands on its own economics and each one reduces the load on the next.
Hygienic and regulatory sign-off
Every product-contact surface is specified to the standard the plant and its auditors require: stainless steel 316L as the default for wetted plate circuits, electropolished finishes where the process demands it, gasketed rather than copper-brazed heat exchangers on any product-contact side, orbital welding with material certification, and full-bore sanitary valves with no dead legs. Pressure equipment is supplied against PED 2014/68/EU or ASME VIII as the destination market requires. In practice the heat pump never touches product — it heats an intermediate circuit through a plate exchanger, so the product path and the HACCP plan are unchanged.
Commissioning, training and the support model
Guaranteed COP at your duty point, not a catalogue maximum. Temperature mapping and validation on the process side. Operator and maintenance training for your own technicians. Remote monitoring. And a written statement of what we do and do not support locally — given up front, rather than discovered during a breakdown at 02:00 in a production run.
The eight objections we get asked first
"Will this affect product safety?"
No, and the reason is structural rather than promissory. The heat pump produces a heating medium; it does not touch product. Heat reaches the product through a plate heat exchanger on the utility side, so the product path, the materials in contact and the HACCP critical control points are all exactly what they were before. What does matter is control accuracy: where the heat is used for a thermal process, the temperature must be held and recorded to the specification. That is an instrumentation and commissioning item, and it is the one we spend most engineering time on.
"What about our retort at 121 °C?"
It stays on the boiler. Not because of temperature — a heat pump can reach 121 °C — but because a retort needs pressurised saturated steam as the heating medium, which industrial heat pumps at this class do not provide reliably. The realistic substitution is everything around it: CIP, pre-rinse, jacket preheat and basket washing, which on a canning line is a substantial share of the steam load. Scope it that way from the start rather than discovering the constraint during commissioning.
"The grid can't take it."
Fair, and it is the most common reason a good project dies. A continuous 60–100 °C duty does need real electrical capacity, and in several of the markets on this page the transformer is the constraint rather than the economics. Mitigation is a staged design sized to your existing headroom, captive or solar generation to displace daytime compressor load, and an honest electrical scope in the quotation. We size to available capacity, not to the theoretical requirement.
"How long is the payback?"
Be sceptical of anyone promising under a year without qualification. Published case studies range from under six months to eight years, and that spread is the gas-to-power ratio and the availability of waste heat, not vendor optimism. In practice the binding constraint is usually the customer's own approval hurdle rate rather than the arithmetic. Phasing the project so Stage 1 carries a short payback is the standard answer, and it is the answer we recommend first.
"Is this really cheaper than a gas boiler?"
Only if your fuel-to-power ratio and your waste heat availability both favour it — and on some markets they do not. Use the calculator above with your own contract prices. If it comes out marginal, we will say so, and we will look at heat recovery first, because recovering heat that is already being thrown away is almost always cheaper than buying a machine that makes it.
"Why not an electric steam generator?"
Because it converts electricity to heat at an efficiency of about 0.98, where a heat pump delivers three to five units of heat per unit of electricity. An electric steam generator is genuinely better in three specific cases: below roughly 200–500 kg/h of steam, below about 2,000 running hours a year, and where full redundancy is non-negotiable. On a continuous base load it loses on running cost by a factor of three to five. We will tell you which side of that line your duty falls on.
"What about the refrigerant?"
This is a real compliance question, not a marketing one. The EU F-Gas regulation has already banned the export of equipment containing refrigerants with a global warming potential of 1,000 or more since March 2025, and further bans on high-GWP refrigerants in self-contained equipment start in 2027 and 2030. Natural refrigerants — R290 propane, R1234ze, CO₂ and ammonia — are where the industry is going. We will state the refrigerant, the charge, the applicable classification and the ventilation and detection design in the quotation. It should not be a surprise at the installation stage.
"What about service and spares?"
A heat pump for a plant running 6,000 hours a year needs a defined support model with a named local capability. We supply the control architecture, the spares philosophy and remote monitoring, and we work through local partners who hold the spares list and the service history. Where local service cannot be guaranteed we say so up front, because that is a question every serious integrator asks first and it deserves a straight answer.
Frequently asked questions
Which food and beverage processes can a high temperature heat pump actually cover?
Commercially, the 60–100 °C band — which is the large majority of a food plant's process heat load. That covers clean-in-place and thermal sanitation at 70–85 °C, low-temperature and high-temperature short-time pasteurisation side circuits at 63–90 °C, blanching at 90–105 °C, the first effect of a multi-effect evaporator at 65–75 °C, batch cooking and pan boiling, and tunnel and belt drying at 60–90 °C. Above 100 °C, steam generation at 110–150 °C is available with materially lower coefficients of performance and requires waste hot water to be worth doing. Routine operation above 150 °C does not exist commercially today.
Can it replace my boiler completely?
No, and framing it that way is a mistake. Industry survey work puts the largest commercial steam heat pumps at around 2 MW while the average boiler in a surveyed food or textile plant was nearly 18 MW — whole-facility electrification is not a realistic proposition this decade. The realistic and bankable pattern is partial electrification: the heat pump carries the base load and the boiler becomes a peaking and standby unit for high-pressure retorts and any duty above 120 °C. In practice this is a better outcome for the customer than a boiler deletion, because a boiler that runs as standby instead of base load lasts considerably longer.
Does it affect food safety or hygiene?
The heat pump never contacts product, so the product path and the HACCP plan do not change. The heat reaches product through a plate heat exchanger on the utility side, and every wetted surface is specified to the applicable sanitary standard — 316L stainless as the default, electropolishing where the process requires it, gasketed rather than copper-brazed construction on product-contact sides, orbital welding with material certification, and full-bore sanitary valves with no dead legs. The genuine compliance focus shifts to control accuracy: where heat is used for a thermal process, the temperature must be held and recorded to specification, which is a commissioning and validation item rather than a hygiene one.
What about retort sterilisation at 121 °C?
Retort stays on the boiler, and the reason is worth understanding precisely. Commercial sterility for low-acid foods is defined by a time–temperature integral referenced to 121.1 °C, and that definition is about the curve the product experiences, not the source of the heat — a valid F₀ can be achieved by any source that delivers the profile. The reason the retort does not convert is narrower: it operates under pressure with saturated steam as the heating medium, and industrial heat pumps in this class deliver hot water or superheated steam rather than reliably pressurised saturated steam at the required quality and rate. Everything around the retort — CIP, pre-rinse water, jacket preheat and basket washing — can and should be electrified.
How is the COP of a high temperature heat pump determined?
COP is output heat divided by input electricity, and it is a strong function of the temperature lift the machine must achieve. At a nominal 25 °C ambient, typical industrial performance runs from about 4.6–5.5 at 40–55 °C delivery, down to 3.2–4.0 at 85–95 °C, 2.7–3.4 at 100–110 °C, 2.1–2.8 at 115–130 °C and 1.5–2.0 at 140–150 °C. Real figures depend on condenser approach, source temperature, compressor selection and part-load behaviour, which is why we ask for a guarantee at your duty point rather than quoting a catalogue maximum.
What heat sources can feed the machine?
Five in a food plant, plus ambient air as the fallback: CIP effluent and cooling-water bleed at 30–50 °C, which is the largest and cleanest and yields COP 5 and above through a heat exchanger; condensate return above 80 °C, where a closed loop typically captures 85–90 % of generated condensate and cuts the feedwater heating load substantially; flash and secondary steam at 105–120 °C, effectively free at the point of generation and usually the best source on a site with an evaporator; dryer exhaust at 80–120 °C, which is usually discharged but can be condensed and returned as usable heat; and refrigeration condenser heat at 40–60 °C from the plant's own cold chain, running continuously with nowhere to put its heat. The last of these is the one that food plants most often overlook, and it is free.
How much of the boiler's load can realistically be taken?
On a plant with a well-designed CIP and pasteurisation estate, the 60–100 °C band typically carries the majority of the process heat and it is the band the heat pump serves best. What the number will not tell you in advance is how much of it is genuinely continuous. Take a survey of the CIP skid's running hours against the pasteuriser's duty cycle against the plant's own production calendar, and the answer becomes clear. Where a plant is dominated by batch operations with long idle gaps, a buffer vessel changes the answer materially — and it is worth evaluating before concluding the project is too small.
What about the refrigerant and the regulations?
It is a legitimate engineering question and it should be answered in the quotation, not at the installation stage. The EU F-Gas regulation already bans from March 2025 the export of equipment containing refrigerants with a global warming potential of 1,000 or more, and further bans on high-GWP refrigerants in self-contained equipment follow in 2027 and 2030. Natural refrigerants — R290 propane, R1234ze, CO₂ and ammonia — are where the industry is going, and each carries different installation requirements: R290 is a flammable fluid requiring ventilation, leak detection and possibly classified electrical equipment; ammonia is non-flammable but toxic and needs material separation from copper. Where a plant has restricted access to plant rooms, this often determines the architecture, and it is cheaper to know it at the quotation stage.
What happens in a power outage?
The heat pump is a compressor-driven device, so it stops with the power. For a plant running continuous shifts this must be designed for: thermal storage sized to ride through the outage profile, and retained boiler or electric boiler capability on standby. This is one of the strongest arguments for keeping the boiler rather than deleting it. Where a site has captive generation or solar, compressor load can be shifted to generation windows, and where the site has a large cold load there is often a natural opportunity to run a heat recovery loop that keeps the hot side alive through an outage.
What about service and spares?
A heat pump for a plant running 6,000 hours a year needs a defined support model with a named local capability and a held spares list. We supply the control architecture, the spares philosophy and remote monitoring, and we work through local partners who hold the service history. If a market has no such partner, we say so before the quotation rather than after. We would rather decline a project than ship a machine into a plant that cannot be maintained, because the reputational damage lands on both of us and on the technology.
Does this work in my country?
The engineering is not country-specific — the physics of a vapour-compression machine does not care where the plant is. What is country-specific is the business case, and it reduces to two numbers: your fuel-to-power price ratio and your grid's carbon intensity. Where both are favourable, a heat pump wins on arithmetic alone. Where they are not, the case usually comes from something else: a mandated emissions limit, a subsidy for a named technology, a fuel supply that is expensive or politically exposed, or simply the fact that the plant already has heat going to waste.
We will run the same two-variable screening for any site, and we will tell you when the answer is that the boiler stays. What we will not do is quote a payback from a market average, because that number is a property of your specific tariff and your specific waste heat — not of the technology. Where a plant is better served by a hybrid arrangement — solar thermal collectors, thermal storage and a heat pump working together under digital control, with the boiler retained as standby — we will scope and price that rather than sell you a single machine that will not do the whole job.
Get a sized scheme from your own data
We do not quote from a per-tonne rule of thumb. Send us the following and we will return a sized system per series, projected COP at your duty point, estimated savings, payback range and the electrical scope — with every assumption written down.
- Twelve consecutive months of fuel and electricity bills
- Your process heat demand — CIP skid size and running hours, pasteuriser capacity and temperature, evaporator duty, dryer exhaust temperatures, steam header pressure and flow
- Production schedule — tonnes per day by product and shift, and the seasonal pattern
- Water and steam sources — condensate return temperature and quality, effluent temperature, flash steam availability, dryer exhaust volume and temperature
- Electrical — transformer rating, spare capacity, existing boiler capacity and header pressures, and any captive generation
- Compliance — destination market, required sanitary standard, and any audit regime you are subject to
Sources and methodology
- IEA — Heat Pump Monitor (2026) and Renewables for Industry (2025): industrial heat pump commercial temperature limits, CAPEX multiples versus gas and coal boilers, and the COP threshold above which heat pumps become competitive.
- IPCC (2006) — Fuel Combustion Emission Factors, Tier 1: natural gas 0.2022 kgCO₂e/kWh (NCV basis).
- Ember — Yearly Electricity Data (2025), via Our World in Data and Helgi Library: grid emission factors for Indonesia, Vietnam, Thailand, Bangladesh, Kazakhstan, Uzbekistan, Turkey, South Africa, Brazil and Chile.
- Cammesa (2025) and ANEEL — Brazilian industrial electricity tariffs and the electricity-intensive profile of juice concentration. CONE (2025) — Chile's electricity price composition and the unbundling of the regulated tariff into energy, capacity and distribution components that made a 30 % price rise possible in 2025. National Energy Regulator of South Africa (2026) — Eskom tariffs including the 240.28 c/kWh average and the 123 c/kWh off-peak band.
- ESDM Indonesia (2026) industrial tariffs I-3 and I-4; Ministry of Energy and Mineral Resources on the HGBT special gas tariff and its seven qualifying industries, which do not include food and beverage. PeroVietnam / IEEFA (2026), PV GAS LPG cylinder pricing and pipeline gas rates, Vietnam Ministry of Industry and Trade decisions 1279/QD-BCT and 963/QD-BCT on time-of-use tariffs. EPDK Turkey (2026-04) industrial tariff revision and natural gas increase. ERC / PEA Thailand 2026 time-of-use tariff schedule and the designated-factory energy conservation subsidy rules, which name heat pumps as an eligible measure. BERC Bangladesh (2026-06) industrial tariff revision and the 2025-04 industrial gas price increase. Kazakhstan Ministry of Energy commodity gas price ceilings by region, and Uzbekistan Cabinet Resolution 243 (2026-05) on electricity and industrial gas tariffs.
- ACEEE / NREL — Industrial Heat Pumps: Electrifying Industry's Process Heat Supply (2022): dairy pasteurisation modelling and simple payback below two years where the power-to-gas price ratio is favourable.
- Apparel Impact Institute — Clean Heat in Textile Manufacturing: Lessons on Steam Heat Pumps to Date (2025–2026): 5–8 year payback band, the ~2 MW commercial steam heat pump ceiling against an ~18 MW average boiler, and the pattern of targeted process-by-process electrification.
- Tetra Pak — Integrated Heat Pump system launch (2025-11-26) and Dairy Processing Handbook: pasteurisation heat recovery performance and the finding that roughly 80 % of dairy plant energy goes to steam and hot water.
- Tetra Heat Pump / Promethean Energy (2026) — F&B process temperature range table, and the published in-range / not-served process list for retort, spray drying and frying.
- Danfoss (2025) — Gulpener brewery 1.5 MW installation, 90 °C water and 130 °C 1 bar clean steam, total energy reduction 75 %; R290 and R600a high-temperature compressor data.
- Carbon Trust / UK DESNZ Industrial Energy Efficiency Accelerator (2025–2026) — Hepworth brewery independent verification: 86 % energy reduction on the boiling stage, 91 % CO₂ equivalent reduction, 65 % cost reduction at COP ≈ 6.
- GEA (2026) — Intermalt Vietnam malt house: 12 MW heating, 60 °C supply, annual mean COP 5.22, approximately 2,000 t CO₂ saved per year.
- UNIDO — Decarbonizing the Industrial Food Sector: Coal Zero by Green Steam (CZ–GS), A2D Facility (a2dfacility.unido.org/node/159), project stage INITIATED, scheduled March 2026 to October 2028: an industrial food processing site in South Africa combining solar thermal collectors (Absolicon), a high-efficiency mechanical vapour recompression heat pump, waste heat recovery and a digital twin, delivering clean steam on a heat-as-a-service model. Stated objectives are approximately 2,754 tCO₂e avoided and more than four tonnes of coal displaced per day, with twelve further industrial plants identified as replication candidates. Partners: TCS, Energineering, Green Line Africa, Absolicon Solar Collector, MG Sustainable Engineering, University of Derby, Broad Reach Energy. Note: these are the project's stated targets, not measured results.
- AtomZero / Colorado State University — New Belgium Brewing air-source 165 °C steam heat pump, ASHRAE 2026 Winter Conference: payback under two years against electric boiler, currently supplying 30–40 % of site steam.
- EHPA (2026) — Guadalajara brewery heat pump award nomination, Johnson Controls with Heineken and Siemens, 85 °C process water.
- FDA — 21 CFR Part 110 (Current Good Manufacturing Practice), Part 113 (low-acid canned foods), Parts 174–178 (indirect food additives). EU Regulation (EC) 1935/2004 on materials in contact with food. PED 2014/68/EU on pressure equipment.
- 3-A Sanitary Standards, Inc. — General Requirements (00-02) third edition, 2026-02-13; and EHEDG Guidelines, including Guideline 2 on joint integrity and the revised Guideline 28 on water use in food and beverage plants.
- EU Regulation (EU) 2024/573 on fluorinated greenhouse gases and the UNEP Kigali Amendment to the Montreal Protocol: refrigerant phase-down timelines, the March 2025 export ban on GWP ≥ 1,000 equipment, and the differing 2028 freeze dates for Central Asian parties.
- Jaber's Energy / DOE EERE steam supply share by industry sector; IndexBox (2026) Asia-Pacific gas boiler market split by end use — used only for the relative ranking of steam-intensive F&B segments.
- HETAPRO — Catalogue: Industrial High Temperature Heat Pumps (Ver. 20261015) and product pages for MT-A2W, MT-W2W, HT-A2W, HT-W2S, HT-A2S and MT-A2A.
Method note. Figures are presented as published by the source named. Where a figure comes from a commercial market report rather than a primary statistical or regulatory source, it is used for directional ranking only. Where a value could not be verified against a primary source, the field is left blank rather than estimated. Country-level electricity and fuel prices move; the ratios matter more than the absolute values, and your own contract prices will beat any published figure.